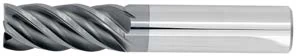
HEM end mills for high efficiency milling
Majac Mills HEM end mills are made for high efficiency milling: a long axial and short radial depth of cut on dynamic or trochoidal toolpaths. 5, 6 and 7 flutes in ultra high performance carbide, mostly ALL4 coated, with or without chipbreakers.
Best for: Dynamic and trochoidal toolpaths in steels, stainless and cast iron.
Sizes available
Pick a diameter to see every High Efficiency Milling tool in that size in the tool finder, with flutes, lengths and coatings.
Starting speeds and feeds
Surface speed (SFM) ranges and the chip load per tooth for a 1/2" diameter tool, from the Majac Mills speeds & feeds guide. On HEM toolpaths, raise the chip load to make up for radial chip thinning. For other sizes, RPM, feed rate and chip thinning, use the speeds & feeds calculator.
| Material | SFM, ALL4 | Chip load (in/tooth), 1/2" |
|---|---|---|
| Aluminum & Aluminum Alloys | 900–1,800 | 0.0045 |
| Copper & Copper Alloys | 525–1,275 | 0.0035 |
| Brass & Bronze | 375–900 | 0.0035 |
| Cast Iron (soft) | 375–950 | 0.004 |
| Cast Iron (hard) | 150–475 | 0.003 |
| Ductile Iron | 200–900 | 0.003 |
| Malleable Iron | 275–850 | 0.004 |
| Low Carbon Steels | 350–900 | 0.004 |
| Medium Carbon Steels | 200–675 | 0.003 |
| Steels Hardened to 35 Rc | 190–545 | 0.0025 |
| Steels Hardened to 50 Rc | 90–275 | 0.0015 |
| Mold Steels | 300–725 | 0.003 |
| Tool Steels | 175–525 | 0.003 |
| Stainless Steels (soft) | 300–525 | 0.003 |
| Stainless Steels (hard) | 150–475 | 0.002 |
| Monel & High Nickel Steel | 75–250 | 0.003 |
| Titanium (soft) | 125–475 | 0.003 |
| Titanium (hard) | 50–195 | 0.002 |
| Nickel-Based High Temp Alloys | 50–175 | 0.0017 |