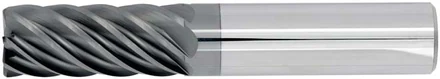
HTAS end mills for stainless steel & high-temp alloys
Majac Mills HTAS (High Temp Alloy & Stainless) end mills use a special high-cobalt carbide grade and an ALL4 coating to stand up to the heat of stainless steels and heat-resistant alloys, and they work well in general steels too. For conventional and HEM toolpaths, with 4 to 7 flutes, longer lengths of cut and chipbreaker options.
Best for: Stainless steel, titanium and nickel-based alloys such as Inconel; also general steels.
Sizes available
Pick a diameter to see every High Temp Alloy & Stainless tool in that size in the tool finder, with flutes, lengths and coatings.
Starting speeds and feeds
Surface speed (SFM) ranges and the chip load per tooth for a 1/2" diameter tool, from the Majac Mills speeds & feeds guide. On HEM toolpaths, raise the chip load to make up for radial chip thinning. For other sizes, RPM, feed rate and chip thinning, use the speeds & feeds calculator.
| Material | SFM, ALL4 | Chip load (in/tooth), 1/2" |
|---|---|---|
| Aluminum & Aluminum Alloys | 900–1,800 | 0.0045 |
| Copper & Copper Alloys | 525–1,275 | 0.0035 |
| Brass & Bronze | 375–900 | 0.0035 |
| Cast Iron (soft) | 375–950 | 0.004 |
| Cast Iron (hard) | 150–475 | 0.003 |
| Ductile Iron | 200–900 | 0.003 |
| Malleable Iron | 275–850 | 0.004 |
| Low Carbon Steels | 350–900 | 0.004 |
| Medium Carbon Steels | 200–675 | 0.003 |
| Steels Hardened to 35 Rc | 190–545 | 0.0025 |
| Steels Hardened to 50 Rc | 90–275 | 0.0015 |
| Mold Steels | 300–725 | 0.003 |
| Tool Steels | 175–525 | 0.003 |
| Stainless Steels (soft) | 300–525 | 0.003 |
| Stainless Steels (hard) | 150–475 | 0.002 |
| Monel & High Nickel Steel | 75–250 | 0.003 |
| Titanium (soft) | 125–475 | 0.003 |
| Titanium (hard) | 50–195 | 0.002 |
| Nickel-Based High Temp Alloys | 50–175 | 0.0017 |